
Hot-dip galvanising is the default finish for cable trays that live outdoors or in industrial air. Pioneer fabricates the tray first — cutting, punching, forming — and only then galvanises it, so every edge, hole and fitting is coated.
HDG vs pre-galvanised GI vs powder coated
| Finish | How it is made | Cut edges and holes | Best for |
|---|---|---|---|
| Hot-dip galvanised (HDG) | Finished tray dipped in molten zinc after fabrication; thick, metallurgically bonded coat | Coated — zinc reaches edges, slots and the inside of holes | Outdoor and industrial plants, refineries, substations, pipe racks, humid plant rooms |
| Pre-galvanised GI | Sheet galvanised in the coil before fabrication (IS 277 / EN 10346), 80 / 120 / 200 / 275 GSM | Bare steel at cut edges and punched holes, protected only by the adjacent zinc | Dry indoor areas — buildings, offices, electrical rooms |
| Powder coated | Mild steel HR sheet (IS 1079) with a baked organic coat, any RAL colour | Covered while the coat is intact; a chip exposes steel | Indoor dry areas, colour-coded and visible runs |
For scale: 275 GSM pre-galvanised sheet carries roughly 20 µm of zinc per side. The HDG perforated tray we submitted for laboratory testing measured 92.4–97.6 µm, average 95 µm — several times thicker, and zinc protects steel roughly in proportion to its thickness.
IS 2629, IS 4759, ISO 1461 and ASTM A123
- IS 2629 — the Indian recommended practice for hot-dip galvanising of iron and steel: cleaning, pickling, fluxing and dipping.
- IS 4759 — the Indian specification for hot-dip zinc coatings on structural steel and allied products.
- ISO 1461 (BS EN ISO 1461) — the international specification for galvanised coatings on fabricated articles. For steel 1.5–3 mm thick it asks for a mean coating of at least 55 µm.
- ASTM A123 — the US equivalent, called up on NEMA-format specifications.
Pioneer galvanises trays to IS 4759 / ISO 1461 / ASTM A123 and reports coating thickness per lot. The published laboratory reports also cover Preece uniformity (3 dips, no copper deposit), hammer adhesion and 24 hours of neutral salt spray to ASTM B117 with no rust.
Where HDG cable trays are used
- Refineries, petrochemical and chemical plants — pipe racks and process-area cable routes.
- Power plants, switchyards and substations.
- Solar plants and other outdoor electrical runs exposed to sun and rain.
- Water and wastewater treatment plants, pump houses and humid plant rooms.
For coastal splash zones or chemical vapour that attacks zinc, step up to SS 316L or FRP.


HDG cable tray data sheet
| Tray types and models | Perforated: HR CTHDP 1002. Ladder: HR CTHDL 2002. Wire mesh: hot-dip galvanised after fabrication. |
|---|---|
| Base steel | Mild steel HR sheet to IS 1079 (TATA / JSW) |
| Galvanising | After fabrication, to IS 4759 / ISO 1461 / ASTM A123; coating thickness reported per lot |
| Widths | Perforated 25, 40, 50, 75, 100, 150, 200, 250, 300, 400, 450, 500, 600 … up to 1200 mm; ladder 25, 50, 75, 100, 150, 200, 250, 300, 400, 450, 500, 600 … up to 1250 mm |
| Heights | 15, 25, 50, 75, 100, 150, 200, 250, 300 and 400 mm |
| Lengths | 2500 mm standard; 3000 mm on request |
| Sheet thickness | 1.2 mm (18 SWG), 1.6 mm (16 SWG), 2.0 mm (14 SWG), 2.5 mm (12 SWG) and 3.0 mm, as per IS 1852 |
| Hardware | Hot-dip galvanised couplers with M8 hot-dip galvanised [SS 304] nuts and bolts |
| Tolerances | Length ±10 mm, width ±3 mm, height ±2 mm, thickness ±0.2 mm (IS 1852) |
| Standards and tests | UL certified; IEC 61537:2023; NEMA VE 1; load tested at an NABL-accredited laboratory |
Specification clause for your BOQ
Copy it into your BOQ or specification and adjust; words in [brackets] are alternatives. The ladder version is on the ladder cable tray page.
Outdoor — hot-dip galvanised
Outdoor, semi-outdoor, humid and industrial areas
1. Cable trays for outdoor, semi-outdoor and humid areas shall be perforated type, fabricated from mild steel HR sheet to IS 1079 and hot-dip galvanised after fabrication to IS 4759 / ISO 1461 [minimum average coating 86 µm where specified].
2. Sheet thickness shall be 2.0 mm for trays up to 300 mm wide and 2.5 mm for trays 450 mm wide and above [or as per the cable tray schedule], with dimensional tolerances as per IS 1852.
3. Tray width and height shall be as per the cable tray schedule; standard height 50 mm [75 / 100 mm where scheduled].
4. All cutting, punching and drilling shall be completed before galvanising; site-cut edges shall be touched up with zinc-rich paint.
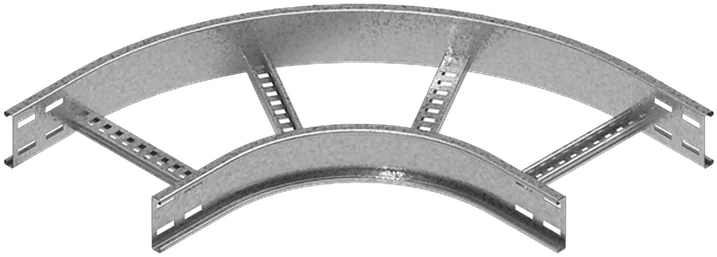
5. Fittings shall be factory made from the same material and thickness and galvanised after fabrication.
6. Couplers shall be hot-dip galvanised with M8 hot-dip galvanised [SS 304] nuts and bolts.
7. Covers shall be provided on runs exposed to direct sun and rain [where scheduled], 1.6 mm thick, galvanised after fabrication.
8. Trays shall be tested to IEC 61537 [NEMA VE 1 where specified] for safe working load at the scheduled support span; load test reports from an NABL-accredited laboratory shall be submitted.
9. Make: Pioneer Cable Trays or approved equivalent.
Why Pioneer
HDG is easy to claim and easy to check. We publish the laboratory numbers and give you coating readings for every lot.
- UL certified cable trays, declared to IEC 61537:2023 and load tested for NEMA VE 1.
- Tested at an NABL-accredited laboratory — load–deflection, zinc coating, salt spray, tensile and chemical reports are published as a PDF.
- Manufacturing since 1994 at our own plant in Pirangut, Pune, which turns out up to 8,000 metres of tray a day.
- Supply across India by road from Pune, and export FOB Nhava Sheva (JNPT, Mumbai).
- Quotation within 24 hours of your BOQ, with the data sheet your consultant needs.